Increasing energy costs, increasingly stringent environmental regulations, increasing production costs and fierce global competition are the driving forces for changes in the building materials/metallurgical industry, which requires continuous optimization of the industry’s calcination (sintering), grinding process, and pollutant emission control technology levels.
Sequoia industrial is a carbon industry chain company. Our company is committed to developing low-carbon footprint process equipment/processes in the building materials/metallurgical industry, combined with our strong local production and manufacturing capabilities to promote this goal.
Our mission is to focus on the pressures and challenges that customers are concerned about, and through key technological innovations, provide customers with competitive building materials and environmental protection solutions and services, and continue to create maximum value for customers.
Frequently Asked Technical Questions
Q1. What is Sequoia's core technical mission on the cement and pyro-processing energy transition?
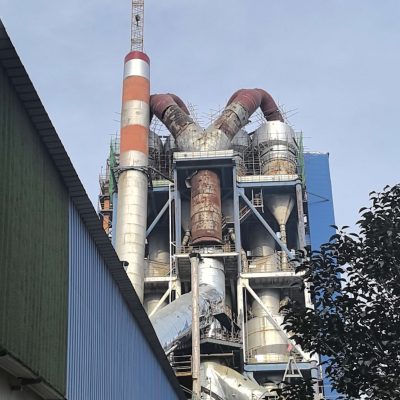
The mission is to make existing cement and lime pyro-lines 10–25% more energy- and carbon-efficient without full kiln replacement — through bolt-on retrofits (cyclone recuts, calciner geometry, kiln-inlet constriction, burner tuning) and fuel substitution (biomass, RDF/SRF, sludge drying). A 5000 t/d clinker line at ~3300 kJ/kg-clinker retrofitted toward ~3000 kJ/kg saves roughly 18 GJ/h and ~1.3 t CO₂/h, equivalent to ~110 kt CO₂/a at 7500 h operation, directly targeting the IEA Cement Roadmap 2030 gap of −20% CO₂ intensity against 2020.
Q2. How does the gypsum-to-acid route fit the sustainability mission?
China generates ~80 Mt/a of phosphogypsum and tens of Mt of FGD/titanium gypsum that are landfilled at high remediation cost. The Bogue decomposition route (CaSO₄·2H₂O + coke at 1150–1250 °C) converts this waste into merchant-grade H₂SO₄ (contact process, two-conversion-two-absorption, >99.5% SO₂-to-SO₃) and a CaO-rich clinker additive that displaces limestone calcination. Each tonne of processed gypsum avoids ~0.4 t of limestone calcination CO₂ and removes a stockpiled hazardous residue — the dual goal of ‘waste-to-acid + calcium co-product’.
Q3. What does 'engineer-led, not contractor-led' mean in practice?
Every retrofit is anchored by a measured heat and mass balance and CFD/cold-flow verification rather than by copying a generic layout. Guarantee values are written into the contract (outlet dust concentration, pressure drop, specific heat consumption, NOx at the stack), and commissioning is performed by the same engineers who did the audit. This is the opposite of lump-sum turnkey where performance is untested until production — Sequoia’s diagnostic-first model caps downside risk.
Q4. What is the near-term carbon-reduction portfolio?
Four pillars: (1) preheater/kiln energy retrofit (best-available −5 to −10% thermal energy); (2) alternative-fuel co-firing up to 30–60% thermal substitution rate with moving-floor storage and RDF preparation; (3) ultra-low NOx via combustion tuning + SNCR/SCR to <50 mg/Nm³; (4) solid-waste co-processing (sludge, biomass, hazardous waste) and membrane-based leachate ZLD. Together these move a typical greenfield-equivalent line toward the 2030 sector target without capital-heavy new kiln builds.
An expert in pyroprocess and solidwaste recovery . Responsible for the Marketing and Support of Sequoia Industrial with over 14 years in this field. I am determined that our sustainable products and services will be at the forefront of the solution for the generations to come.

 中文
 English



Comments (0)