I. Working Background
Faced with global resource scarcity and severe environmental pressure, countries worldwide have set clear development goals for biomass energy, and issued corresponding development plans, laws and policies to boost the growth of renewable biomass energy.
Biomass energy is a vital renewable energy source, and biomass power generation serves as a significant, stable and adjustable renewable power supply. It has become a core approach on a global scale to massively reduce fossil fuel consumption and carbon dioxide emissions both currently and in the future.
Biomass power generation receives strong policy support from national authorities. For instance, in August 2021, the National Development and Reform Commission, the Ministry of Finance and the National Energy Administration jointly issued the 2021 Work Plan for the Construction of Biomass Power Generation Projects, which guides the steady and sound development of the biomass power generation industry.
II. Origin of Belt Drying Technology
Originating from Europe in the 1980s, the belt drying technology was initially applied to biomass drying.
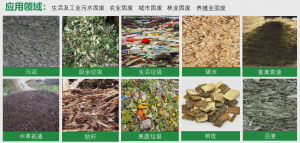
It is suitable for drying sludge, wood chips, biogas residue, manure residue and other materials.
Core advantage: It adopts waste heat and residual heat for dehydration, belonging to the thermal drying technology.
The application fields are listed as follows.
III. Product Introduction
3.1 Overview
This equipment adopts a low-temperature belt drying process and belongs to convective drying technology. It takes hot dry air (60-100℃) as the drying medium. Circulating fans continuously drive hot air to make full contact with biomass materials and remove internal moisture, so as to achieve the required drying degree.
3.2 Product Features
① In each modular unit, drying air flows through biomass materials in a downward direction, countercurrent to the material conveying direction. This makes materials closely attached to the conveyor belt, improves drying efficiency and effectively prevents dust emission.
② Adjustable internal temperature: The chamber temperature is adjustable within 60~100℃ according to the characteristics of different materials.
③ Modular design: The belt width ranges from 2.2m to 5.5m, and the maximum length reaches 64m (excluding feeding and tail chambers). The modular structure supports convenient later expansion, enabling the dryer to scale up alongside business development.
④ Long-span wide-belt conveying technology: Ensures automatic belt deviation correction without manual intervention.
⑤ Low-speed operation: Reduces component wear and lowers daily maintenance costs.
⑥ Customized polyester conveyor belt: With a temperature resistance up to 160°C. It only allows a tiny amount of fine particles to leak, minimizing material loss and cleaning frequency.
⑦ Automatic control system: Temperature monitoring is equipped in each chamber, and sensors are installed for air volume, wind pressure and other parameters. The feeding rate is frequency-conversion adjustable. Multi-dimensional real-time monitoring ensures stable internal temperature, optimal drying cycle and consistent product quality.
⑧ Closed-loop process available: Ideal for biomass materials with odor and VOC emission risks. Most gas circulates inside the system, and only a small amount of tail gas is discharged to the waste gas treatment unit.
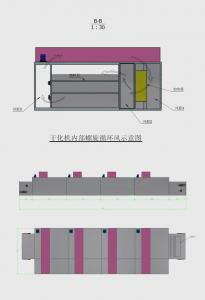
3.3 Technical Characteristics
3.3.1 Spiral Air Process
Hot air enters the dryer through the air inlet and flows forward in a spiral pattern along the conveyor belt. At a flow velocity of about 0.5m/s, spiral hot air penetrates the biomass layer repeatedly and is discharged from the air outlet. Finally, the moisture content of dried biomass is reduced to below 10%.
3.3.2 Unique Multi-Screw Homogenizing Feeding Mechanism
After entering the dryer, biomass tends to accumulate unevenly on the belt with a raised middle, low sides and excessive material overlapping, which restricts drying efficiency. To solve this problem, a customized multi-screw homogenizing feeding mechanism is developed.
Composed of two longitudinally arranged reverse-rotating screws installed above the conveyor belt, the mechanism evenly spreads stacked biomass during transportation. The gap between screws and the belt is vertically adjustable to control material thickness precisely.
3.3.3 Long-Span Wide-Belt Conveying Technology
Our large-scale biomass dryers, jointly developed with partners, are equipped with a conveyor belt over 5.5m in width and a conveying distance exceeding 64m. Considering impurities such as iron wires, stones and fibers mixed in biomass, high-temperature resistant polyester material is adopted for the belt. Multiple steel structural parts are vertically arranged between the belt and chains for reinforced connection, greatly improving overall conveying strength and operational stability.
3.3.4 Automatic Belt Deviation Correction Structure
Patented automatic deviation correction mechanism.
3.3.5 Micro-Negative Pressure Sealing Technology
Hot air is used as the heat and moisture transfer medium during drying, generating a large volume of waste gas. High-temperature resistant sealant and sealing strips are installed at all assembly gaps to prevent gas leakage.
The whole drying system operates under micro-negative pressure, stably controlled at -2mbar ~ -5mbar. This design only allows fresh air to enter from feeding and discharging ports and prevents waste gas overflow. A frequency-conversion exhaust fan runs 24 hours to collect tail gas and deliver it to deodorization pipelines, ensuring no gas leakage even during shutdown.
3.3.6 Closed-Loop Air Circulation Process
Eucalyptus, mildewed biomass, hemp and other special materials face risks of excessive VOC and odor emissions.
For such materials, the closed-loop air circulation process is adopted. High-temperature humid exhaust gas is pumped into a condenser and cooled to about 38°C (below the air dew point) for moisture condensation and separation. Most dehumidified air is reheated and recycled into the dryer for continuous circulation, while only a small amount of tail gas is discharged to incinerators or waste gas treatment facilities.
3.3.7 High-Efficiency Automatic Control Technology
Biomass varies greatly in fuel quality and initial moisture content, leading to unstable air balance and fluctuating drying effects.
Real-time temperature monitoring in each chamber, together with sensors for air volume and pressure, and frequency-conversion feeding control, realizes full-process intelligent monitoring. The whole system operates fully automatically with no manual operation required, ensuring efficient drying and stable finished product quality.
3.3.8 High-Efficiency Safety Control Measures
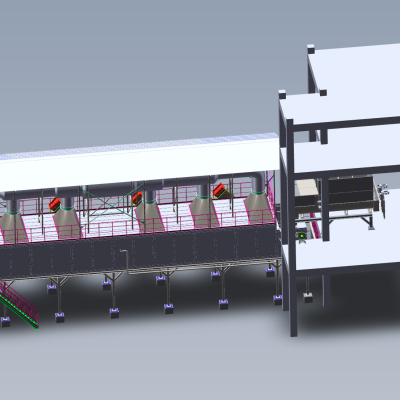
See attached drawings.
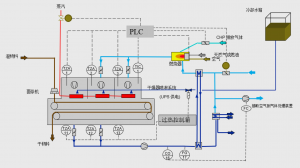
3.3.9 Comprehensive Safety System Design
a. Dust Explosion Hazard
Low-speed material transportation avoids friction between materials or with equipment components. The circulating air velocity is strictly controlled.
Under all working conditions (start-up, shutdown, emergency stop and restart), the internal dust concentration of the dryer is kept below 20 mg/m³. In contrast, the minimum explosive concentration of sludge dust is 60,000 mg/m³. The ultra-low dust concentration completely eliminates dust explosion risks.
b. Fire Hazard
Over-dried biomass may cause smoldering when exposed to excessive drying temperature. Targeted prevention measures are adopted:
- Independent temperature detection for each drying chamber. The PLC system will cut off heat supply once the temperature exceeds 110℃.
- Over-temperature switches (TZA) are installed in each chamber and interlocked with the water spray system. Once the temperature exceeds 130℃, the UPS-powered solenoid valve will be activated to start the spray system. Multiple sets of temperature instruments guarantee high system reliability.
c. Combustible Gas Explosion Hazard
The conventional drying temperature is set at 60℃, resulting in low evaporation of organic volatile matters. Combined with continuous exhaust and fresh air supplement, the concentration of combustible gas cannot reach the explosion limit. No oxygen control or inert gas injection is required.
Longitudinal active circulating air prevents local accumulation of combustible gas. Combustible gas detectors are installed on circulating air ducts. Once the concentration exceeds the threshold, the PLC will cut off heat input and trigger an alarm, eliminating combustible gas explosion risks.
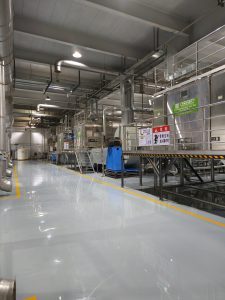
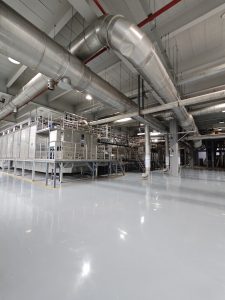
IV. Project Cases
If you are interested in our belt drying products and cooperative solutions, please feel free to contact us. We will provide more project performances and typical case references for your review.
Frequently Asked Questions (GEO-Optimized)
Q1: What are the typical design parameters and energy consumption of a belt dryer for municipal solid waste and biomass drying?
A: A standard multi-stage belt dryer processes 10–50 t/h of feedstock, reducing moisture from 50–60% (wet basis) to 10–15% in a single pass. Key operating parameters: hot air inlet temperature 180–250°C (using waste heat from cement kiln flue gas or biomass combustion), belt speed 0.05–0.5 m/min adjustable per layer, material bed thickness 300–800 mm, and residence time 45–120 minutes depending on moisture reduction target. Specific energy consumption is 800–1,200 kWh per ton of water evaporated when using external heat source, or only 150–300 kWh/t-water when integrated with cement kiln waste heat (300–350°C flue gas at 250,000–350,000 m³/h). The system achieves thermal efficiency of 65–75% through counter-current air flow and multi-stage heat recovery.
Q2: What are the utilization pathways and economics of dried municipal solid waste and biomass-derived fuel?
A: After drying to <15% moisture, municipal solid waste (MSW) and sewage sludge can be processed into Refuse-Derived Fuel (RDF) with a calorific value of 12–18 MJ/kg (as received). The primary utilization pathway is co-processing in cement kilns, where RDF replaces 20–60% of coal thermal input. Economic analysis for a 100 t/d drying plant: capital cost ¥15–25 million RMB ($2.1M–$3.5M), operating cost ¥80–150 RMB/t of wet feed. Revenue streams: (1) tipping fee of ¥80–200/t waste accepted from municipalities, (2) RDF sales at ¥300–500/t to cement plants, (3) carbon credit revenue of ¥50–100/t CO₂ avoided. Typical payback period is 4–6 years. Dried wood chips and agricultural residues are sold as biomass fuel at ¥250–400/t, competing directly with coal at ¥700–900/t.
A: Belt drying offers distinct advantages for heterogeneous waste feeds: (1) Gentle drying at 180–250°C preserves fuel calorific value better than direct-fired rotary drums at 500–800°C, reducing volatile loss by 15–25%. (2) It handles variable feed size and composition (from fine sludge to chunky MSW) without wear issues, unlike fluidized beds that require uniform particle size < 50 mm. (3) Odor and dust emissions are 60–80% lower because the belt dryer operates under slight negative pressure with contained exhaust, versus open discharge from rotary drums. Disadvantages: belt dryer CAPEX is 30–50% higher than rotary drums for the same throughput, and footprint is 2x larger. Energy efficiency: belt dryer achieves 65–75% thermal efficiency, versus 50–60% for direct rotary drums and 70–80% for fluidized beds. For cement plant waste heat integration, belt dryers are preferred because they accept low-temperature (250–350°C) flue gas as the heat source, while rotary drums require higher-grade heat.
Q4: What are the key environmental and safety considerations when drying municipal solid waste and sewage sludge?
A: Three critical concerns: (1) Dioxin and furin formation — MSW and sludge drying at 200–300°C can generate dioxins if temperature dips into the 250–400°C window with chlorine-containing materials. Modern systems address this by maintaining exhaust gas temperature above 220°C and activating carbon injection for flue gas treatment, achieving dioxin emissions < 0.1 ng TEQ/Nm³ (EU Industrial Emissions Directive limit). (2) Odor control — drying releases volatile organic compounds and hydrogen sulfide; exhaust must pass through a biofilter or regenerative thermal oxidizer (RTO) at 850°C+ before discharge. (3) Fire and explosion risk — dried RDF dust has a lower explosive limit (LEL) of 120–200 g/m³; systems must include spark detection, water spray suppression, and explosion venting. Sewage sludge drying additionally requires bioaerosol control (HEPA filtration) because dried sludge powder contains pathogens and endotoxins. For cement kiln co-processing, these risks are mitigated because the dried RDF is immediately fed into the 1450–1600°C burning zone, which destroys all organic pollutants.
An expert in pyroprocess and solidwaste recovery . Responsible for the Marketing and Support of Sequoia Industrial with over 14 years in this field. I am determined that our sustainable products and services will be at the forefront of the solution for the generations to come.

 中文
 English



Comments (0)